
In pharmaceutical laboratories and food processing areas, environmental cleanliness, precise temperature control, and regulatory compliance are directly linked to product quality and public safety. Standard building panels often fail to meet the stringent requirements of these sectors. This is where specialized solutions from a trusted manufacturer make a critical difference.

Why Pharmaceutical and Food Industries Require Specialized Insulated Panels?
The core requirements of these industries can be summarized as follows:
- Aseptic Environment: Must effectively prevent the accumulation of microorganisms, mold, and dust.
- Precise Climate Control: Ensures production, storage, and research processes occur at constant temperature and humidity.
- Regulatory Compliance: Materials must meet international hygiene standards such as GMP and FDA.
- Durability and Easy Cleaning: Surfaces must withstand frequent, rigorous washing and disinfection protocols.
Core Product Series for Clean and Controlled Environments
Our product portfolio is designed to meet the specific needs of different applications within these demanding sectors.
Cleanroom Panels: The Core Barrier for Aseptic Environments
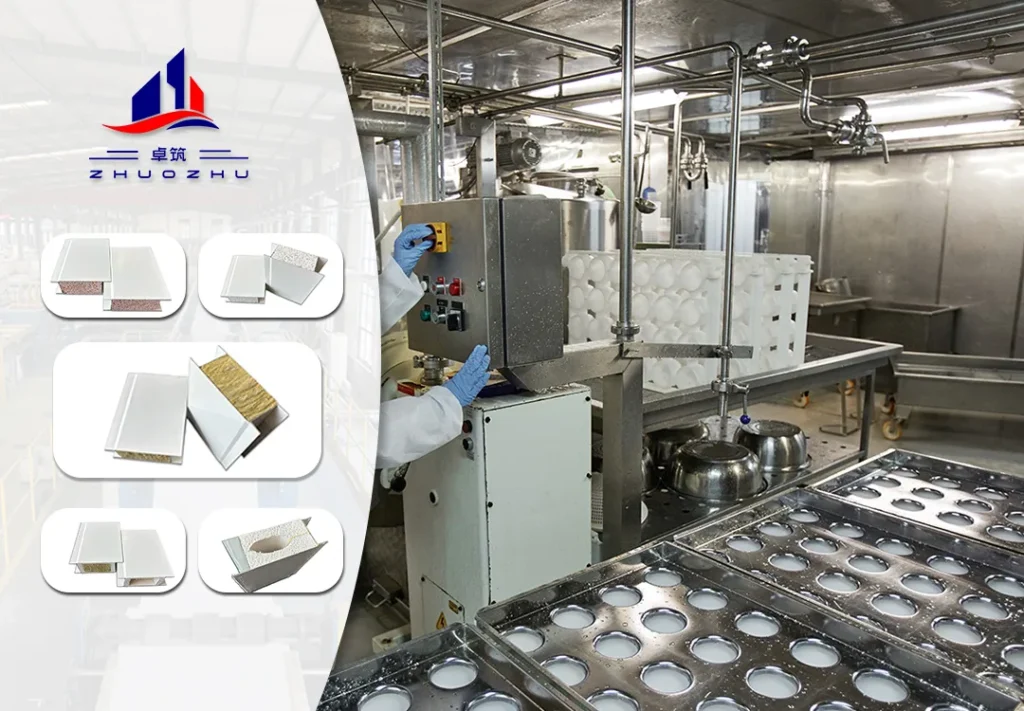
The cleanroom panel series is a primary choice for pharmaceutical labs and high-end food processing zones. These panels feature unique sealed joint designs that ensure tight connections, effectively preventing air leakage and the ingress of contaminants.
- MgO Cleanroom Panels: Offer excellent fire resistance and moisture resistance, completely free of harmful substances, making them ideal for high-standard clean areas.
- Rockwool Cleanroom Panels: Combine superior fire resistance (Class A non-combustible) with good thermal insulation, commonly used in areas with strict fire safety requirements.
- FEPS Cleanroom Panels: Provide a cost-effective clean zone solution while remaining lightweight and offering efficient thermal insulation.
PUR/PIR Sandwich Panels: Superior Thermal Efficiency
For cold room areas or constant-temperature workshops with high demands for energy efficiency, PUR/PIR sandwich panels are the preferred choice. Their extremely low thermal conductivity helps maintain stable indoor temperatures, significantly reducing energy consumption. Whether used as wall panels or roof panels, they create a highly efficient and energy-saving building envelope.
Cold Room Panels: Safeguarding Food Preservation
Our cold room panels are an upgraded version of standard PUR/PIR and rock wool sandwich panels, featuring greater thickness and more precise connection systems for enhanced thermal performance and superior airtightness. The panel surfaces often come with hygienic-grade coatings, making them easy to clean and perfectly suited for the stringent requirements of food processing and cold storage facilities.
Five Core Advantages of Choosing Our Solutions
- Compliance & Safety: Products are designed in strict accordance with industry standards, ensuring your facility passes certifications smoothly.
- High-Efficiency Insulation: Core materials like
PUR,PIR, andRockwoolprovide consistent and durable thermal performance, reducing operating costs. - Robust & Durable: The panels offer structural stability, strong impact resistance, and a long service life.
- Easy Installation: The modular design from our
factorysignificantly improves construction efficiency for projects worldwide. - Globally Trusted: As a reliable
Chineseexporter, our products are shipped worldwide and trusted by international clients.
Selecting the right insulated panels for pharmaceutical and food industries is a strategic decision impacting quality, safety, and efficiency. With comprehensive product portfolios and technical expertise, the right insulated composite panel solution for your cleanrooms, laboratories, and cold storage facilities is available. Contact us today for expert product advice and quotations from a leading manufacturer.
